The global Block Forming Machine market is becoming more important as cities demand faster, denser, and more resource-efficient construction. Grand View Research identifies continuing growth in the global concrete blocks market, supported by urbanization and infrastructure investment. Fortune Business Insights also highlights automation, durability, and sustainable materials as major construction-equipment trends.
The numbers look encouraging. The details matter more. A modern plant may run beside a dusty aggregate yard, producing hundreds of uniform blocks each hour. Yet output alone does not prove quality. Buyers must examine vibration systems, mold accuracy, hydraulic stability, curing compatibility, energy use, and after-sales support. Reports from MarketsandMarkets and Research and Markets point toward smarter automation and rising demand for efficient production lines. However, published market estimates differ noticeably. That variation deserves attention, not blind confidence.
Dr. Peter C. Taylor, a respected concrete-technology specialist, has repeatedly emphasized that quality depends on controlling both materials and production processes. His principle applies directly here: “Quality begins with control of the materials and the process.” The best manufacturers understand this connection. They do not sell steel frames alone. They engineer repeatable results. This overview compares leading Block Forming Machine manufacturers worldwide through equipment capability, field experience, technical support, customization, and reliability. Some rankings remain debatable. They should. A manufacturer with impressive specifications may still disappoint when spare parts arrive slowly or local aggregates behave differently. Practical performance, verified references, and transparent testing provide stronger evidence than glossy brochures.
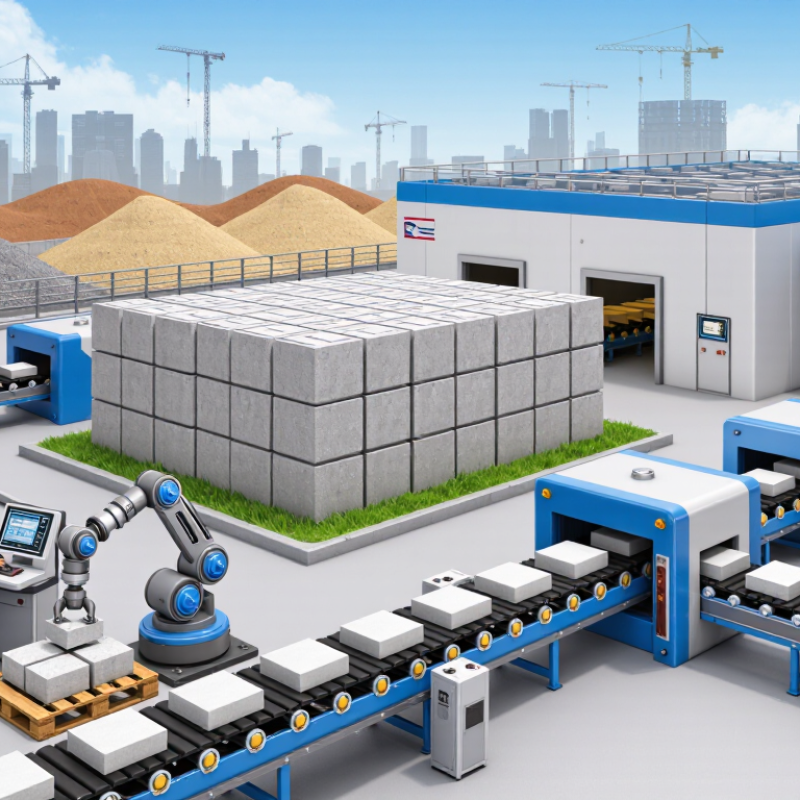
Block forming machines are industrial systems that compact concrete, cement, aggregates, and water into repeatable masonry units. They may use vibration, hydraulic pressure, or both. A mould defines the block’s dimensions, while controlled pressure improves density and surface consistency. In practical production, operators monitor moisture, cycle time, mould wear, and curing conditions. Small changes can create visible cracks.
Their role extends beyond simple shaping. They support faster output, reduce manual handling, and help standardise wall components for housing, pavements, and infrastructure. The International Energy Agency reports that buildings consume about 30% of global final energy and produce around 26% of energy-related emissions. Efficient block production cannot solve this problem alone, but consistent units may reduce material waste and construction rework. The 2023 Global Status Report for Buildings and Construction also identified buildings and construction as responsible for 37% of global energy and process-related emissions. That figure makes production choices more important.
A machine’s value depends on the whole process. Poor aggregate grading, excessive water, or weak curing can defeat precise moulding. A polished machine is not magic. Producers should verify compressive strength, dimensional tolerance, and energy use through documented testing. The assumption that higher output always means better performance is convenient, but incomplete. A slower cycle may produce stronger blocks and fewer rejects. Regional standards and site conditions still matter. Real expertise appears in these details, not only in headline capacity.
Top Block Forming Machine Manufacturers Worldwide
Key Technologies Used in Modern Block Forming Equipment
Modern block forming equipment combines hydraulic pressure, vibration control, automated material feeding, and digital monitoring. These systems help produce consistent blocks with fewer dimensional defects. On a production floor, the difference is visible: stable vibration creates sharper edges, while uneven moisture causes weak corners and surface cracks.
The International Energy Agency’s 2023 Cement Report identifies cement production as responsible for about 7% of global energy-related and process CO2 emissions. This pressure is influencing equipment design. Servo-driven motors, variable-frequency drives, and automatic curing controls can reduce wasted energy during pressing and handling. Small improvements matter.
Very small adjustments help.
Sensors now monitor mould pressure, vibration frequency, pallet position, and mix moisture. A programmable logic controller can adjust feeding time within seconds. The World Bank’s What a Waste 2.0 report projects global solid waste to reach 3.4 billion tonnes annually by 2050. This supports greater use of recycled aggregates, although material consistency remains difficult. Recycled content can change block density from one batch to another. That assumption deserves testing.
Artificial intelligence is entering quality inspection through camera-based surface analysis. It can detect chipped edges faster than manual checks, but dust and poor lighting still create false alarms. The technology is useful, not flawless. Equipment buyers should examine energy consumption, calibration records, mould-change time, and after-sales technical support before comparing machine capacity claims.
Comparing global block machine manufacturers requires more than counting advertised cycles per hour. Start with verified output, not brochure capacity. The Global Cement and Concrete Association reports that the world uses about 14 billion cubic metres of concrete annually. This scale makes stable production valuable, but only when blocks meet consistent dimensions, density, and strength. Ask for independent test records, mould-change time, vibration frequency, and reject rates. A short factory trial can reveal more than a polished presentation.
Energy and material efficiency deserve equal attention. The International Energy Agency reported that cement production generated about 1.5 gigatonnes of direct CO2 emissions in 2022. A machine that reduces cement waste, curing losses, or unnecessary vibration may lower both operating costs and environmental impact.
Compare kilowatt-hours per production cycle, water use, aggregate tolerance, and compatibility with recycled materials. Check whether the manufacturer supports recognized quality systems, documented commissioning, operator training, and spare-parts availability across regions.
Lifecycle support is often underestimated. Review warranty terms, remote diagnostics, response times, and the cost of critical components. ISO 9001 certification can indicate controlled processes, but it does not prove machine performance. Request customer references from climates similar to your own. Do not rely only on the highest output figure. It may depend on ideal aggregates and experienced operators. No scorecard is perfect. A practical comparison should weight reliability and local service, even when the initial price looks less attractive.
Block forming machine manufacturers are shaped by the needs of their home markets. In East Asia, producers often focus on automated lines, precise molds, and high output. Their equipment suits large projects with stable electricity and trained operators. European manufacturers usually emphasize safety systems, energy efficiency, and long service life. Their machines often support strict quality controls and detailed documentation.
South Asian producers commonly develop practical machines for varied budgets and changing site conditions. Simple hydraulic systems can be easier to repair locally. Some models also handle frequent movement between construction sites. In North America, manufacturers often prioritize robust frames, digital monitoring, and compatibility with regional building standards. Service networks matter as much as machine capacity.
Africa, Latin America, and the Middle East show different priorities. Dust protection, water availability, fuel costs, and uneven infrastructure can affect equipment selection. Regional manufacturers may offer compact machines with accessible components. That can reduce downtime when imported parts arrive slowly. Yet local production is not automatically better. Quality testing, mold accuracy, operator training, and documented output still require careful review.
The details matter.
A reliable buyer should compare vibration performance, curing conditions, spare-part access, and technical support. Factory visits can reveal more than polished catalogs. One weakness remains common: manufacturers sometimes advertise maximum capacity instead of realistic daily production. This figure deserves independent verification before investment.
| Region | Primary Manufacturing Hubs | Common Machine Configurations | Typical Rated Output | Most Produced Block Types | Key Market Drivers | Important Compliance Considerations |
|---|---|---|---|---|---|---|
| East Asia | China, Japan, South Korea and Taiwan | High-speed hydraulic presses, pallet circulation systems, automatic batching lines and robotic handling cells | Approximately 5,000–20,000 standard concrete blocks per 8-hour shift for fully automated lines | Hollow blocks, solid blocks, paving units, kerbstones and masonry units | Large-scale urban construction, infrastructure investment, export-oriented equipment production and automation demand | Applicable national construction standards, electrical safety rules, guarding requirements and local emissions controls |
| South Asia | India, Pakistan, Bangladesh and Sri Lanka | Manual and semi-automatic hydraulic machines, mobile units, vibration presses and compact production lines | Approximately 300–5,000 blocks per 8-hour shift, depending on automation and mould configuration | Concrete masonry units, hollow blocks, solid blocks, interlocking pavers and roadside products | Affordable housing, road construction, local manufacturing, replacement of fired clay products and demand for low-capital equipment | Regional standards for compressive strength, dimensional tolerance, workplace safety and electrical installation |
| Southeast Asia | Vietnam, Indonesia, Thailand, Malaysia and the Philippines | Semi-automatic and automatic hydraulic presses, mobile machines and integrated batching-and-palletizing systems | Approximately 1,500–12,000 blocks per 8-hour shift for commonly installed commercial systems | Hollow blocks, paving blocks, interlocking units, drainage products and lightweight aggregate blocks | Residential development, industrial parks, transport infrastructure, tropical-climate construction and urban expansion | National product standards, humidity-resistant electrical components, operator protection and site-specific power requirements |
| Europe | Germany, Italy, Spain, Turkey, Poland and the Czech Republic | Precision-controlled automatic lines, multi-layer presses, servo-hydraulic systems and closed-loop material handling | Approximately 4,000–18,000 units per 8-hour shift, with output varying by product size and curing method | High-precision masonry blocks, pavers, kerbs, retaining-wall units and architectural concrete products | Energy-efficient production, renovation, infrastructure upgrades, strict quality control and demand for premium surface finishes | CE-related machinery requirements, EN-based product standards, occupational safety, noise control and energy-efficiency expectations |
| Middle East | Türkiye, the United Arab Emirates, Saudi Arabia, Iran and Jordan | Heavy-duty hydraulic presses, automatic block lines, mobile equipment and high-capacity batching systems | Approximately 2,000–15,000 blocks per 8-hour shift, depending on aggregate grading and automation level | Hollow blocks, thermal-insulation blocks, paving stones, kerbs and large-format masonry units | Large building projects, logistics and industrial zones, infrastructure programs and demand for durable products in hot climates | Local building codes, heat-resistant electrical systems, dust control, aggregate quality and operator-safety requirements |
| Africa | South Africa, Egypt, Nigeria, Kenya, Morocco and Algeria | Mobile and semi-automatic machines, diesel-compatible systems, compact hydraulic presses and modular production lines | Approximately 300–6,000 blocks per 8-hour shift for commonly deployed small and medium-scale equipment | Hollow blocks, solid blocks, paving units, interlocking soil-cement blocks and kerbstones | Affordable housing, public works, local material supply, employment-focused manufacturing and urban population growth | Power reliability, local material testing, dust exposure controls, machine guarding and national construction standards |
| North America | United States, Canada and Mexico | Automated concrete products plants, high-pressure presses, integrated curing systems and computerized production monitoring | Approximately 5,000–20,000 units per 8-hour shift for industrial-scale installations | Concrete masonry units, architectural blocks, pavers, retaining-wall products and specialized landscape units | Commercial construction, infrastructure renewal, landscape products, labor-saving automation and consistent product quality | ASTM-based product testing, OSHA-related workplace safety, electrical codes, accessibility requirements and environmental permitting |
| Latin America | Brazil, Mexico, Colombia, Argentina, Chile and Peru | Manual, semi-automatic and automatic hydraulic machines, mobile units and flexible multi-product mould systems | Approximately 500–10,000 blocks per 8-hour shift, depending on plant scale and product mix | Hollow blocks, structural blocks, pavers, kerbs and interlocking concrete products | Residential construction, municipal infrastructure, housing programs and demand for locally sourced building materials | National technical standards, seismic design requirements in applicable markets, electrical safety and concrete-strength testing |
| Oceania | Australia and New Zealand | Automated pallet systems, high-accuracy presses, compact lines for regional plants and integrated curing solutions | Approximately 3,000–15,000 units per 8-hour shift for commercial production lines | Concrete masonry units, architectural blocks, pavers, retaining-wall products and landscape elements | Residential development, civil construction, landscaping, infrastructure maintenance and demand for durable low-maintenance products | Australian and New Zealand building standards, workplace safety rules, seismic considerations and environmental controls |
Top Block Forming Machine Manufacturers Worldwide
Selecting a Manufacturer for Specific Production Requirements
Choosing a block forming machine manufacturer begins with your actual production target, not a catalog photograph. Define daily output, block dimensions, raw material, curing method, and available floor space. Measure the mold carefully. A machine designed for lightweight blocks may perform poorly with dense paving units.
Review technical evidence from experienced manufacturers. Ask for cycle-time records, dimensional tolerances, vibration settings, and power consumption under similar conditions. Request sample blocks made with your aggregate and cement ratio. Small differences in moisture can change surface quality and demolding stability. Do not guess.
The supplier should explain mold replacement, hydraulic maintenance, control-system training, and spare-part availability. A factory visit can reveal practical details, such as weld quality, protected wiring, and access around the maintenance panels. Check whether technicians can respond within your operating region. That matters during a night-shift breakdown.
Production flexibility also deserves attention. Interchangeable molds, adjustable feeding systems, and automatic pallet handling may support future products. However, extra automation can increase training needs and repair costs. No selection is perfect. I have seen buyers focus on maximum capacity, then struggle with storage, labor, or curing space. Compare the complete operating cost, including electricity, molds, rejected blocks, and scheduled service. References from plants with similar materials are more useful than impressive showroom demonstrations.
Standard concrete masonry units commonly use nominal widths of 100, 150, 200, 250, and 300 mm. Actual widths are typically about 8 mm smaller to allow for mortar joints. When selecting a block-forming machine, manufacturers should confirm mold compatibility, product range, changeover time, and the required production capacity for each target size.
Hein Minnie
Cell nr: +27 (0) 82 564 6501
Email: sale@thecirclemachine.com
Hein Minnie Jnr
Cell nr: +27 (0) 84 284 7234
Email: sale@thecirclemachine.com
Address:
10 Apsey Street,
Heidelberg,
Gauteng,
1441
Bendet Engineering Services (PTY) LTD was established in 1987. Our team of engineers and draughtsman are ready to deliver a complete turnkey solution, from the design phase to commissioning. A dedicated team that consists of electrical, mechanical and industrial engineers, we are able to offer a comprehensive service to our clients.